Benchmarked across moisture equilibrium resilience, tenon-and-mortise structural integrity, and multi-step artisanal lacquering for worldwide hospitality, corporate, and luxury residential deployments.
An authoritative teardown of botanical properties, structural stability index, and precision joinery methods required for high-frequency contract spaces.
Authentic mahogany (Swietenia macrophylla) and select tropical hardwoods remain the gold standard in five-star hotel lobbies, luxury boardroom consoles, and architectural millwork. Unlike softwoods or rubberwood blends that expand across cross-sections, mahogany possesses an exceptionally uniform pore distribution with interlaced cell matrices.
When procured through verified Chinese industrial facilities and established Indonesian workshop clusters, the raw timber undergoes computerized vacuum dehumidification. This suppresses fiber stresses and reduces tangential shrinkage rates to below 4.1%, eliminating splitting in arid Western heating systems.
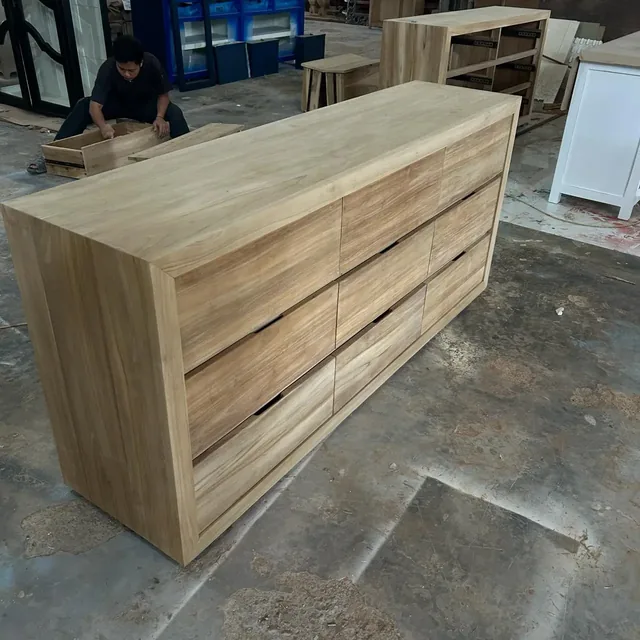
| Evaluation Parameter | Certified Solid Mahogany | Solid Teak Wood (Tectona) | Standard MDF / Wood Veneer |
|---|---|---|---|
| Volumetric Shrinkage Ratio | Low (7.8% green to ovendry) | Ultra-Low (7.0% ovendry) | Unstable under water exposure (edge swell) |
| Structural Load Bearing | Superior (Modulus of Rupture: 80 MPa) | Exceptional (Modulus of Rupture: 95 MPa) | Prone to creep and sag under continuous load |
| Natural Rot & Termite Shield | Class II Durable Heartwood | Class I (High natural tectoquinone oil) | Zero resistance without heavy chemical additives |
| Finish Receptivity | Flawless: Melamine, Duco, Oil Stains | Best for natural wax & PU saturation | Prone to delamination & edge peeling over time |
| Projected Commercial Lifespan | 35+ Years in active hospitality environments | 50+ Years (Indoor & Outdoor) | 3–7 Years before mandatory replacement |
Global supply chains are shifting rapidly. Here are the core structural transformations procurement directors, hospitality specifiers, and retail buyers must prepare for over the next 5 years.
Import regulations like the US Lacey Act amendments and the EU Deforestation Regulation (EUDR) require zero-tolerance proof of origin. Leading factories now integrate digital chain-of-custody tracking from plantation logging concession coordinates directly to bill-of-lading container packages.
The boundary between traditional cabinet-making and modern metallurgy is blurring. Architects are specifying hybrid architectures: solid mahogany facades embedded into powder-coated matte aluminum chassis, hidden carbon fiber stabilizing battens, and wireless inductive charging points milled beneath solid hardwood desks.
Hotel flags are moving away from disposable flat-pack inventory toward solid timber pieces that can be sanded, re-stained, and repaired on-site every 8 to 10 years. Specifying solid mahogany lowers the Total Cost of Ownership (TCO) across a resort's operational lifecycle by over 42% compared to synthetic laminates.
Do not sign purchase contracts until your factory inspection team or third-party auditor verifies these critical workshop capabilities.
Demand real-time temperature and moisture sensor logs. Hardwood timber must spend 18 to 28 days inside steam-assisted kilns to drop core moisture below 10% without cell collapse.
Refuse furniture held together only by pocket screws or MDF staples. Demand true mortise-and-tenon joints, blind dovetails on drawers, and floating breadboard ends on wide tables.
Ensure lacquering occurs inside pressurized positive-air spray booths to eliminate trapped airborne dust. Multi-step sanding (up to 400-grit) between glaze coats is mandatory.
Overseas maritime transit involves high humidity and container condensation. Insist on foam edge protectors, 5-ply corrugated cartons, dessicant silica strips, and fumigated timber crates.
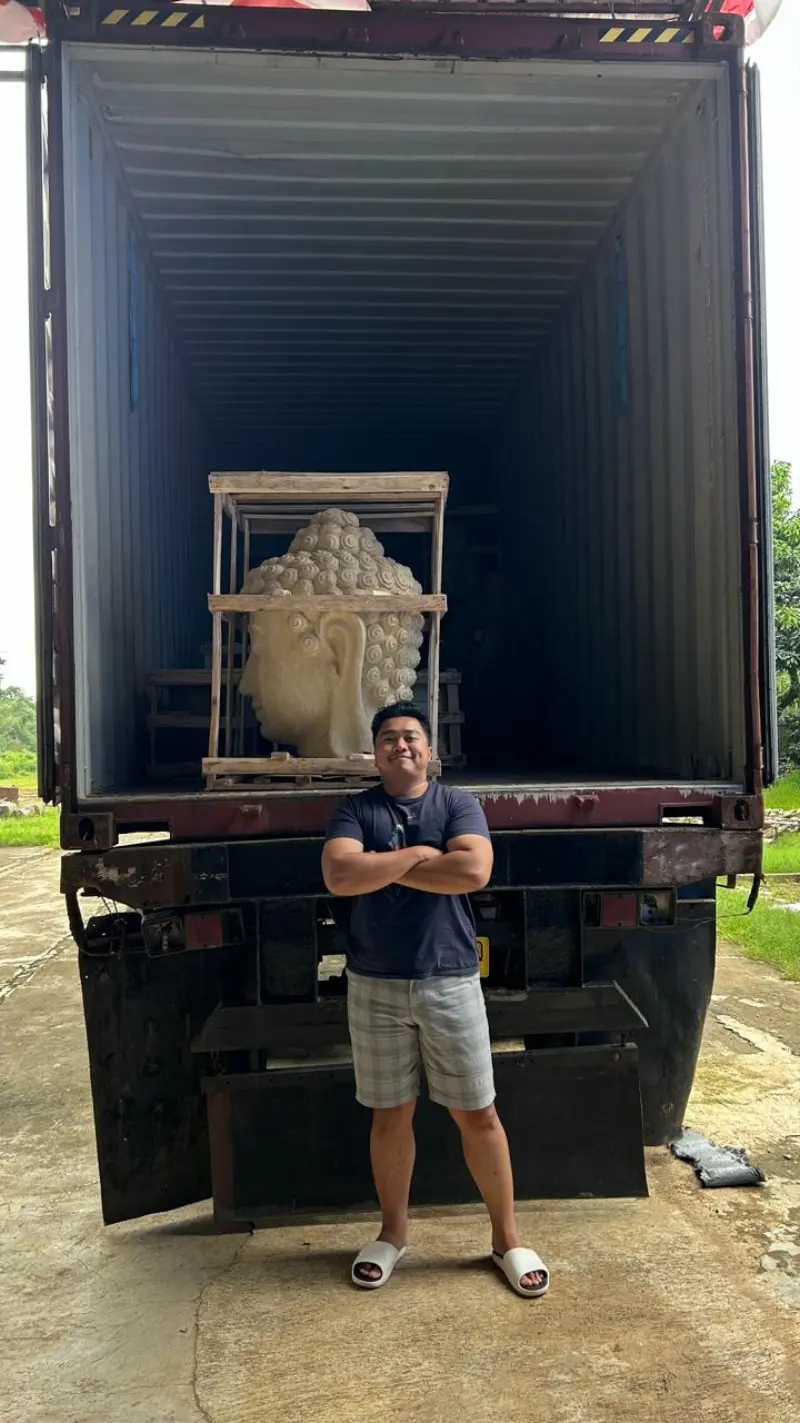
Founded as an authentic family woodworking workshop in 1995, our manufacturing facility has expanded across three decades of direct export trade to prime architectural markets in the United States, Germany, New Zealand, and the United Kingdom.
Unlike trading intermediaries that mark up products by 30% without setting foot on a factory floor, we operate our own production lines: master carvers, seasoned joinery artisans, specialized sanding teams, and dedicated in-house Quality Control/Quality Assurance inspectors.
Definitive answers covering timber legality, custom manufacturing minimums, container logistics, payment structures, and moisture control.
We are a direct manufacturing enterprise with dedicated workshop grounds, cutting yards, drying facilities, and finishing halls established in 1995. When you communicate with our team, you liaise directly with production technicians who understand wood movements, structural joinery, and finish chemistries. This eliminates intermediate broker margins and ensures direct accountability from initial technical drawing to sealed ocean freight containers.
Timber warpage and surface cracking occur when internal moisture content drops rapidly in low-humidity environments. Our factory employs a rigorous two-phase stabilization cycle: natural air-seasoning followed by computer-regulated vacuum kiln drying that stabilizes core moisture levels precisely between 8% and 10%. Furthermore, table tops utilize slotted screw brackets and floating cleat systems, enabling cross-grain movement without cracking the frame.
Yes. Every batch of timber processed in our facilities is 100% legal and verifiable under SVLK (Sistem Verifikasi Legalitas Kayu) certification and FSC chain-of-custody protocols. When exporting to the North American market, all shipments comply fully with the US Lacey Act declaration standards, and European orders include complete documentation proving non-deforestation origin under EUDR frameworks.
Our standard production runs are calibrated for 20ft Full Container Loads (approx. 28–30 CBM), which provides commercial buyers with the lowest freight cost per item. However, for interior designers, boutique hospitality mock-ups, and specialized project trials, we accept consolidated Less-than-Container Load (LCL) orders. Pre-production physical samples can be crafted, finished, and dispatched via air courier within 14 working days from CAD approval.
Bespoke OEM/ODM fabrication represents more than 60% of our annual production. You can submit hand-drawn sketches, project concept mood boards, or detailed DWG/Revit files. Our drafting office confirms structural joint specs, wood species allocations, hardware selections, and finishing nuances in a comprehensive shop-drawing package for sign-off prior to wood cutting.
We provide an extensive range of commercial-grade surface finishes: natural hand-rubbed Danish oil for showcasing authentic wood grain, waterborne low-VOC polyurethane coats for dining surfaces, hard-wax matte sealers, rich dark mahogany/espresso glazes, and opaque Duco enamel lacquer matching any RAL or Pantone color code. Fire-retardant and anti-scratch coatings meeting hospitality specifications are available on request.
For standard project orders, payment terms are typically a 30% deposit upon proforma invoice confirmation to initiate timber allocation and production scheduling, with the remaining 70% balance due upon completion and approval of comprehensive Quality Assurance reports prior to container loading. For multi-container phased developments, staggered container-by-container payment and release schedules are standard practice.
Export packaging complies with international transit drop tests: corners are secured with multi-density high-impact foam guards, surfaces are wrapped in anti-abrasive non-woven polyethylene liners, and cases are enclosed in heavy-duty 5-ply corrugated master cartons. For intricate hand-carved details or tables exceeding 2.2 meters, custom fumigated OSB or solid wood outer skeleton crates provide absolute protection against container shifting.
We welcome international procurement officers, contract specifiers, and third-party testing agency auditors (such as SGS, TÜV, or Intertek) directly at our production workshops. Operating hours are Monday through Sunday between 08:00 and 16:00. Simply schedule an appointment with our sales department prior to your arrival so our engineering lead can accompany you across raw timber logs, machining halls, and finish lines.
Standard manufacturing duration is approximately 4 to 6 weeks for a 20ft container and 6 to 8 weeks for a 40ft High Cube container, depending on the complexity of hand-carved joinery or specialized finish treatments. Confirmed lead times are locked in writing in your formal commercial quotation to safeguard your project critical-path timelines.