
Direct workshop-to-market lines manufactured under strict dimension allowances, kiln-dried moisture stabilization (≤10-12%), and premium grade-A SVLK certified lumber.
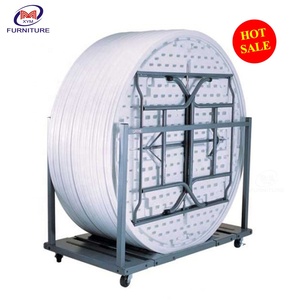
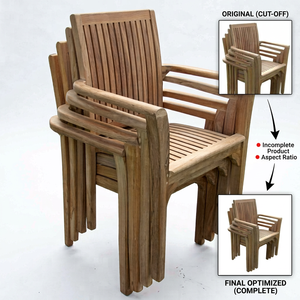
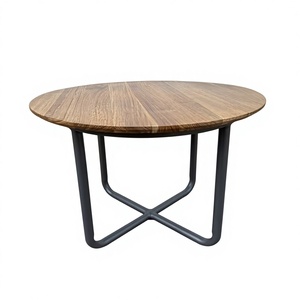
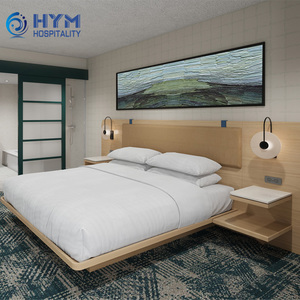
Originating from the historic Jepara woodworking enclave and scaling through China's world-class supply chain orchestration, we bridge artisanal joinery with high-throughput contract manufacturing. Since 1995, our master woodcrafters and finish engineers have executed complex custom credenzas for premier commercial distributors, luxury retailers, and multi-key hospitality brands across North America, Europe, and Australasia.
Unlike rigid mega-factories that restrict procurement to massive identical runs, our production structure allows modular line flexibility. Importers can consolidate bespoke teak sideboards, executive credenzas, matching coffee consoles, and architectural casing within a single project window without bearing exorbitant tooling minimums.
Get a Quote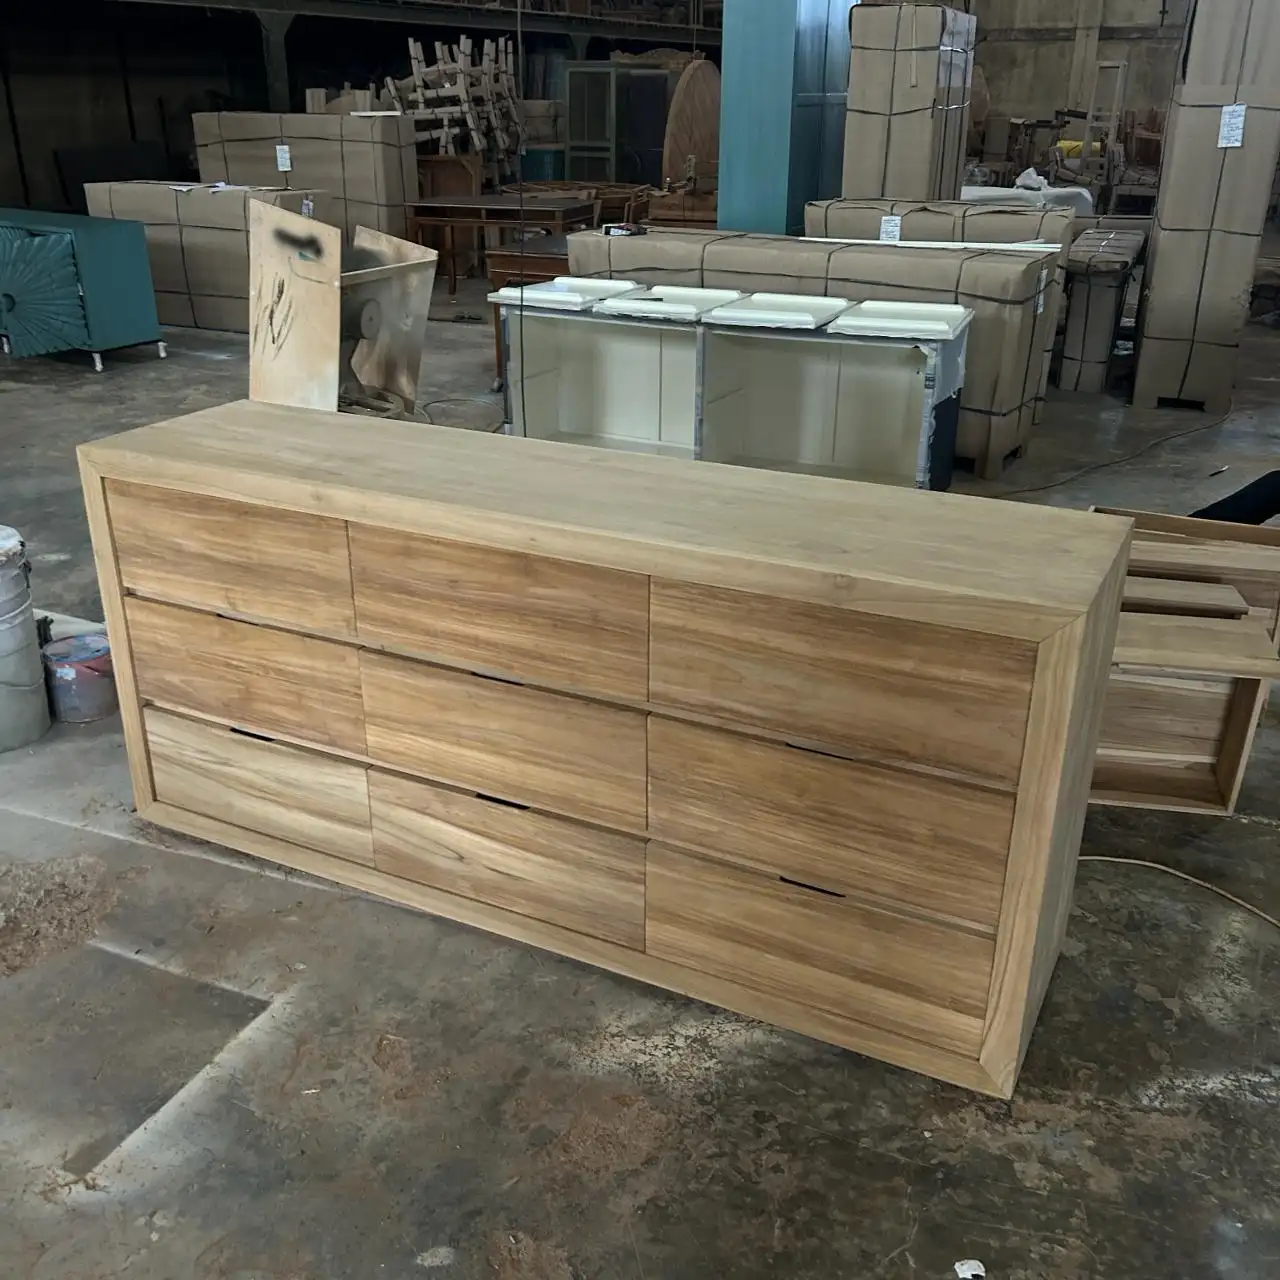
Years Manufacturing & Global Export Experience (Est. 1995)
Traceable Kiln-Dried SVLK Legal Teak & Hardwood Timber
Agile Turnaround per 20ft/40ft Export Container Batch
Tolerance for Uninspected Packing; Dual Gate QA Protocols
Understanding structural deflection limits, silica content dynamics, moisture equilibrium curves, and multi-axis mortise joinery in export casing furniture.
Export failure in solid wood credenzas is almost invariably caused by uneven equilibrium moisture content (EMC). High-end teak (Tectona grandis) exhibits extreme density and intrinsic natural tectoquinones (oils) which retard moisture exchange. Our computerized dehumidification kilns systematically reduce moisture to 10% ± 2%, stabilizing internal cellular tension to prevent catastrophic panel warping, veneer delamination, or drawer binding across divergent climatic transport zones.
A standard 1800mm to 2400mm credenza top experiences significant lateral expansion and contraction across annual seasonal shifts. We engineer floating top panels with sliding expansion buttons, blind dovetails, and haunched mortise-and-tenon structural carcass framework. This enables continuous micro-dimensional breathing without transmitting shearing stress to the drawer banks, sliding tambour tracks, or structural uprights.
Because natural teak contains high natural silica and resin oils, ordinary polyurethane varnishes suffer poor chemical bonding and subsequent flaking. We utilize deep-penetrating specialized polyurethane cross-linkers, matte catalyzed lacquers, and multi-stage hand-rubbed organic oil formulations that preserve natural tactile warmth while meeting stringent European EN 12720 scratch, hot liquid, and ethanol resistance standards.
| Engineering Parameter | Commercial Grade (Standard Market) | Our Institutional Master-Grade Specification | Operational Impact for Importers |
|---|---|---|---|
| Timber Origin & Grade | Mixed sapwood/heartwood, wild unverified cuts | 100% SVLK Certified Heartwood Teak, Grade A/AB | Zero customs clearance holdups; superior color uniformity |
| Moisture Control (EMC) | Sun-dried or fast-air kilned (16% - 20%) | Computerized slow steam kiln-seasoned (10% ± 2%) | Eliminates structural shrinkage, panel splitting, and mold in transit |
| Sub-structure Casing | Stapled chipboard or hollow MDF with paper wrap | Solid teak framing with multi-ply counterbalanced balancing cores | Withstands commercial heavy dynamic loading (>150 kg deflection limit) |
| Hardware Integration | Generic friction tracks, unbranded iron hinges | Concealed soft-close undermount slides (Blum / DTC institutional) | 100,000+ cycle fatigue resistance; zero end-user maintenance calls |
| Pre-Shipment QA Check | Spot audit (1 piece per 20 containers) | 100% full dry-assembly & drawer-action gate inspection | Eliminates onsite installation rework and costly warranty claim liabilities |
Strategic supply chain analysis for category managers, interior procurement directors, and multi-unit hospitality developers navigating global raw material shifts.
Commercial and high-density residential design is moving rapidly from glossy heavy ornamentation to clean, organic, biophilic lines. Fluted fronts, micro-reeded tambour doors, and integrated recessed J-pull handles are displacing applied brass hardware, maximizing natural grain visibility.
Contract buyers now demand credenzas incorporating sintered stone surfaces, sintered quartz inserts, brushed champagne metal aprons, and wireless induction charging stations directly embedded underneath 8mm teak surface tops for executive office applications.
With the European Union Deforestation Regulation (EUDR) taking center stage alongside US Lacey Act provisions, institutional purchasers require full geolocation polygon coordinates for timber concessions. Our automated digital traceability guarantees audited compliance from harvest lot to shipping container.
Skyrocketing ocean freight rates and warehouse handling overhead have triggered intense demand for high-end credenzas built with pre-indexed German eccentric cam fasteners and blind metal dowels, enabling flat-pack container stuffing efficiency without compromising structural solidity upon assembly.
Critical insights for global buyers regarding lead times, custom shop drawings, moisture stability, and cross-border shipping logistics.
We operate direct production lines and specialized artisan workshops with roots going back to 1995. Our manufacturing structure integrates dedicated master woodcrafters, precision joinery machinists, surface treatment specialists, and full-time QA/QC engineers. You negotiate, calibrate specifications, and confirm tolerances directly with the workshop builder.
All solid lumber undergoes multi-phase dehumidification kiln-drying to achieve a standardized moisture content of 10% ± 2%. During fabrication, we incorporate stress relief relief cuts on expansive undersides, elongated slotted screw holes with brass ferrules, and floating panel frames that accommodate natural seasonal equilibrium expansion without splitting.
Our standard baseline container lead time is 4 to 6 weeks from technical shop drawing approval and deposit receipt. While a full 20ft/40ft container yields optimal ocean freight amortization per cubic meter (CBM), we routinely accommodate lower-volume LCL project orders and consolidated multi-product mixed containers for boutique developers and retailers.
Yes. We specialize in contract OEM and bespoke ODM manufacturing. Simply submit your architectural elevations, AutoCAD files, 3D renderings, or dimensional sketches. Our engineering office translates your concepts into production-ready shop drawings indicating internal joinery, grain orientation, cable-management conduits, and exact hardware specs for written sign-off.
All teak and hardwood timber is procured under strict SVLK (Sistem Verifikasi Legalitas Kayu) legal certification frameworks, fully cross-compliant with the US Lacey Act, European EUTR/EUDR requirements, and Australian Illegal Logging Prohibition laws. We provide V-Legal documentation, complete fumigation certificates, Certificates of Origin (COO), and verified packing lists.
Every credenza undergoes a comprehensive 5-layer export packaging protocol: (1) protective poly foam wrap against abrasion, (2) edge-guard perimeter protectors along all delicate corners, (3) heavy-density EPE foam buffering around drawer and door faces, (4) double-wall 5-ply corrugated master cartons, and (5) reinforced, heat-treated wooden crates or palletized skids for LCL voyages.
Whether you require a customized line for a luxury retail brand, 100+ room turnkey hospitality cabinetry, or high-velocity container distribution, our engineering and manufacturing teams are equipped to deliver precision craftsmanship on schedule.