
Multi-Function
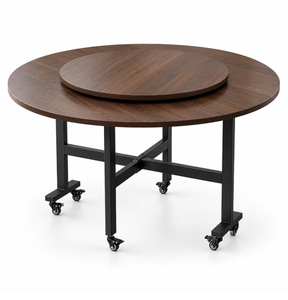
Manufactured under strict timber legality, SVLK-traceable compliance standards, precision mortise-and-tenon framing, and durable multi-coat polyurethane protective seals.
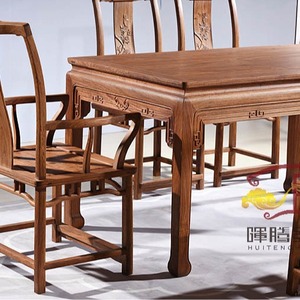
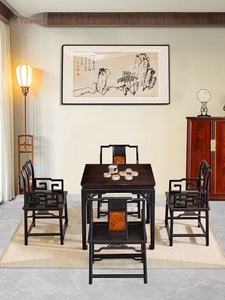
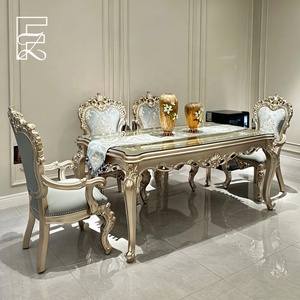
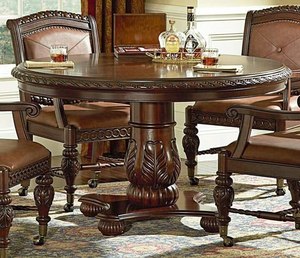
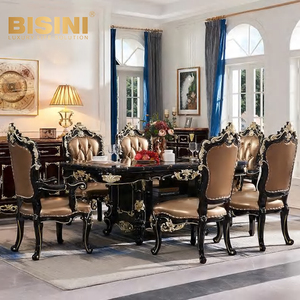
A technical guide for commercial buyers, furniture importers, interior design firms, and hospitality general contractors navigating the mahogany dining supply chain.
Procuring authentic mahogany (Swietenia macrophylla, Khaya senegalensis, and legal Southeast Asian certified reserves) requires strict hygroscopic control. As an anisotropic natural material, mahogany expands across tangential and radial planes based on surrounding relative humidity (RH). Top-tier manufacturing hubs deploy computerized high-frequency vacuum kiln drying tunnels. Raw timber undergoes controlled multi-stage conditioning over 21 to 28 days to yield a verified 8% to 12% moisture equilibrium. This rigorous pre-processing prevents post-installation joint displacement, surface checking, and structural cupping when shipping across diverse microclimates—from humid coastal regions to dry North American indoor winter heating environments.
High-yield commercial performance demands authentic floating tenon and traditional mortise joinery. While cheap flat-pack alternatives rely entirely on zinc eccentric cam locks and carbon steel bolts—which inevitably loosen under cyclic dynamic loading—commercial hospitality specifications mandate structural wood-to-wood joinery fortified with cold-press thermosetting polyurethane adhesives (PVA Class D4 waterproof standards). For long tables exceeding 2400mm in length, integrated under-table stress-relief kerfs and cold-drawn steel C-channel stabilizers are routed directly into the underside of the mahogany slab, preserving cross-grain dimensional integrity while accommodating natural seasonal movement.
| Performance Metric | Traditional Handcrafted Workshop | Commercial High-Volume Factory | Integrated OEM/ODM Specialist (Our Model) |
|---|---|---|---|
| Timber Certification | Localized documentation, mixed origin | Industrial FSC/SVLK bulk compliance | Direct Chain-of-Custody SVLK & US Lacey Act audit trail |
| Drying Methodology | Air dry / primitive heating kiln (14%–18% MC) | Accelerated steam kiln (10%–14% MC) | Dehumidification vacuum kiln + rest aging (8%–10% MC) |
| Joinery Precision | Manual chiseling, human variance ±1.5mm | Fast KD mechanical fasteners, prone to racking | 5-Axis CNC machined mortise-and-tenon + hand-fitted joints |
| Finishing Technology | Manual NC lacquer / wax wipe | High-speed UV roll-coat line (flat panels only) | Multi-tier electrostatic spray: PU primer + matte acrylic topcoat |
| Order Flexibility | High MOQ or low capacity | Strict container loads (FCL only, single SKU) | LCL consolidate, mixed container SKU, full custom drawings |
Over the 2026–2030 sourcing horizon, B2B procurement patterns are shifting toward three defined technical domains:
• Biophilic Hybrid Engineering: Designers increasingly pair genuine dark-grained mahogany substructures with sintered stone, natural Italian marble slabs, and aircraft-grade aluminum sub-frames. This combination protects high-wear surfaces while retaining the tactile prestige of hardwood bases.
• Low-VOC & Waterborne Polyurethane Systems: Strict cross-border environmental mandates (such as CARB Phase 2, EPA TSCA Title VI, and EU REACH regulations) have rendered traditional solvent-borne nitrocellulose lacquers obsolete. Modern finishing facilities implement ultra-low VOC waterborne polyurethanes and zero-emission natural plant-oil seals that meet indoor air quality standards without masking the chatoyancy and grain depth of mahogany.
• Small-Batch Customization via Distributed Manufacturing: Large importers no longer maintain rigid 1,000-unit inventories of a single SKU. Sourcing preferences have decisively pivoted toward agile workshops capable of delivering mixed-container shipments (LCL or multi-model 20ft/40ft HQ loads), allowing boutique retailers and hospitality interior planners to execute custom architectural drawings with zero tooling penalties.
Unlike trading intermediaries, our integrated operational model eliminates non-value-added brokerage costs while delivering artisan-grade execution backed by over three decades of export leadership.
Every board of teak and mahogany carries comprehensive legal chain-of-custody verification under Indonesia’s national SVLK system and global trade compliance mandates.
Full-time specialized QC/QA inspectors rigorously assess structural joinery, sanding grit uniformity, and moisture content before flat-pack or assembled protective crating.
Provide a reference render, architect’s sketch, or full technical specification. Our master pattern makers translate concepts into finished prototypes with exact dimensional tolerances.
From single-project LCL consolidation alongside your existing regional freight to standard 20ft and 40ft High Cube container loads, our staging team optimizes CBM pack-out efficiency.
Speak directly with technical pattern makers, wood technologists, and export logistics coordinators without intermediary communication barriers.
Practical operational guidelines addressing production timelines, legal certifications, quality assurance gates, and payment security.
We are a direct family-founded manufacturing facility established in 1995. Our direct operational infrastructure incorporates master timber carvers, multi-stage finishers, dedicated structural engineers, and independent QC/QA supervisors. Sourcing directly through our factory floor guarantees transparent material tracking and removes hidden agent markups.
For standard 20ft Full Container Load (FCL) orders, our production cycle spans approximately 4 to 6 weeks from technical drawing sign-off and deposit receipt. For complex custom hospitality joinery or multi-container phased deliveries, a firm staggered shipment schedule is established directly on your formal Proforma Invoice.
All timber inputs are audited under national SVLK (Sistem Verifikasi Legalitas Kayu) certification schemes and comply fully with the United States Lacey Act Amendment and EU Timber Regulations (EUTR). V-Legal export declarations and phytosanitary certificates accompany every commercial bill of lading.
We provide full-spectrum finishing capabilities: raw penetrating teak-oil wax, durable multi-tier polyurethane (PU) sealers in matte (10%), satin (30%), or high-gloss sheens, and specialized solid pigmented Duco coatings. Submit a physical Pantone reference or wood finish sample chip, and our finishing laboratory will formulate an exact color match.
Standard enterprise terms mandate a 30% initial project deposit upon order confirmation. Crucially, each individual container is fully staged, photographed, and made available for third-party auditing (SGS/TÜV or buyer agent inspection). The remaining balance is remitted only after formal QC sign-off and container door sealing.