Engineered for high-traffic contract hospitality suites, residential master lounges, and luxury exterior living. Fabricated to strict international dimensional tolerances with full OEM/ODM prototyping support.
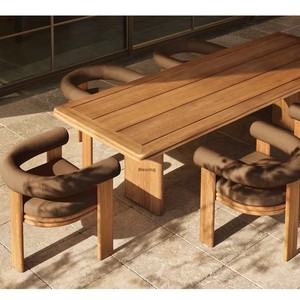
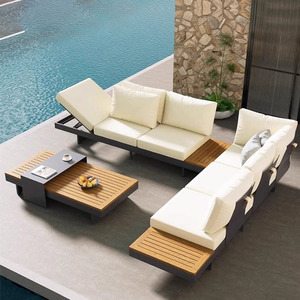
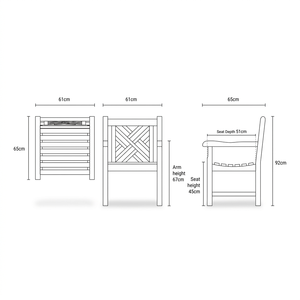
Located on the arterial manufacturing corridor of Jl. Raya Soekarno Hatta (KM.5 No.95) in Jepara, Central Java—the generational epicenter of Indonesian woodworking—Teratai Furniture operates a purpose-built family workshop balancing heirloom artisanal joinery with strict commercial production control.
Unlike monolithic assembly-line factories locked into rigid minimums of thousands per SKU, our manufacturing infrastructure is deliberately structured around agile micro-batching. With an in-house core team of four master woodworkers, five dedicated surface-finishing technicians, and two independent QA/QC inspection engineers (backed by a dynamic scalable sanding and pre-assembly guild), we provide direct, unmediated communication from shop-floor CAD drawings to final maritime crating.
"We eliminate the traditional friction of third-party export brokers. Every millimeter of grain alignment, tenon depth, and finish calibration is confirmed directly by our shop-floor leaders."
Unstabilized tropical hardwoods crack in air-conditioned western climates. Our lumber undergoes controlled dehumidification kilning over 21–28 days to bring core moisture content (MC) to exactly 8%–12%, engineered to withstand the HVAC extremes of North America, Northern Europe, and Australasia without warping.
Every teak accent chair built in our Jepara facility is constructed with true structural mortise-and-tenon joints, reinforced with internally drawn wooden dowels and water-resistant polyurethane or Type 1 structural cross-linking adhesives. No exposed sheet-metal screws in critical structural shear planes.
Strategic market intelligence for commercial furniture importers, contract procurement executives, and hospitality specification groups navigating shifting regulatory and design demands.
Modern luxury interiors and five-star coastal retreats are moving away from monolithic, heavy wooden silhouettes. Global procurement data reveals a 38% year-over-year surge in demand for hybrid accent chairs: pairing organic, SVLK-certified Grade-A teak framing with hand-woven French hexagonal cane (rotan webbing), twisted all-weather Olefin marine cord, and architectural powder-coated metal sub-bases.
With the enforcement of the European Union Deforestation Regulation (EUDR) and heightened stringency in US Customs Lacey Act audits, institutional hospitality developers and public-facing retailers can no longer accept unverified lumber origins. Indonesian SVLK (Sistem Verifikasi Legalitas Kayu) has become an indispensable baseline, verifying plantation legality from government-sanctioned Perum Perhutani forests through export V-Legal declarations.
The boundary between interior living spaces and open-air loggias has dissolved. Commercial buyers increasingly specify accent chairs capable of transitioning between suites and balconies. This requires wood treated to develop a dignified silvery patina if exposed to salt mist, or protected with ultra-matte, non-yellowing, zero-VOC waterborne polyurethane coats that preserve the warm golden hue of virgin teak heartwood.
Rising global holding costs and shifting trend cycles make mega-factory 500-unit single-SKU orders obsolete for boutique interior firms. Sourcing directors are prioritizing specialized workshops capable of producing 10–50 bespoke accent chairs per model within a consolidated 20ft container, incorporating custom seat heights, branded metal badges, and localized fabric upholstery.
While mass producers rely on flat slat profiles, luxury contract buyers demand compound-curved backrests, organic waterfall seat rims, and sculpted joint transitions. The winning formula blends multi-axis rough shaping with traditional Jepara hand-spoke shaving, delivering tactile warmth that mechanical automation alone cannot replicate.
High ocean container tariffs require spatial efficiency. Leading exporters are redesigning solid teak accent chairs with precision mortise-and-tenon knock-down hardware, reducing shipped volume (CBM) by up to 55% while maintaining instantaneous job-site assembly and replacing plastic foam wraps with multi-layer corrugated paper cushions.
Clear, direct answers regarding production logistics, technical wood tolerances, minimums, and commercial payment protection.
We are a direct family-owned manufacturing facility located on Jl. Raya Soekarno Hatta KM.5 No.95 in Jepara, Central Java, operating continuously since 1995. When you contact Teratai, you communicate directly with our workshop management—not a commission-taking intermediary. You are welcome to inspect our timber seasoning, assembly benches, and finishing bays during working hours (08:00–16:00 WIB).
Our standard production runs are optimized around one 20ft container (approx. 28–30 CBM, accommodating roughly 120–180 accent chairs depending on geometry). However, because we champion flexible production, we welcome mixed container orders combining different chair designs, tables, and consoles, as well as LCL (Less-than-Container Load) sample batches from 10 units when consolidated with other Indonesian shipments.
Every piece of teak (Tectona grandis) and mahogany processed in our facility is certified under Indonesia's national timber verification system, SVLK (Sistem Verifikasi Legalitas Kayu). We provide full V-Legal documentation for every export shipment, providing effortless compliance with the United States Lacey Act, European Union EUDR/FLEGT guidelines, and Australian Illegal Logging regulations.
Tropical wood contains high green moisture that must be methodically extracted. We subject our raw dimensioned lumber to 3–4 weeks of progressive kiln drying, monitoring internal moisture until it stabilizes at 8%–12% MC. We leave timber to condition before final sizing, utilizing marine-grade polyurethane joinery adhesives that absorb seasonal equilibrium fluctuations without splitting.
Yes. OEM and ODM bespoke manufacturing represents over 70% of our workshop output. You can submit standard PDF shop drawings, DWG files, 3D renderings, or rough hand-sketches with target dimensions. Our team prepares a technical production review confirming mortise joint tolerances, grain direction, cushion foam densities, and packaging blueprints before cutting sawdust.
For standard container orders, production begins with a 30% project commitment deposit. The remaining 70% balance is invoiced only after our dedicated two-person QC department finishes final inspection and provides comprehensive high-resolution photographic and video proof of the completed order, prior to container stuffing and export clearance at the port of Tanjung Emas, Semarang.
A standard 20ft container of made-to-order teak accent chairs generally requires 4 to 6 weeks of shop-floor production, factoring in kiln drying, multi-stage sanding, joint assembly, and custom finish curing. For repeat collection orders with standard finishes, lead times can be compressed to approximately 3 to 4 weeks depending on ongoing kiln queue capacity.
We offer five standard contract finishing protocols: Fine-Sanded Natural (which naturally weathers outdoors to a silver-grey patina), Deep Penetrating Teak Oil, Non-Yellowing Matte Polyurethane (for high-spill hospitality dining), Melamine lacquer, and opaque solid color Duco sprayed enamel (matched to RAL or Pantone swatches for contemporary hotel branding).
Absolutely. We regularly integrate high-density reticulated quick-dry outdoor foams, client-supplied COM (Customer's Own Material) fabrics, Sunbrella performance textiles, top-grain automotive-grade leathers, natural Indonesian cane webbing, and custom laser-cut PVD-coated stainless steel brackets. All assembly occurs under our single roof to guarantee seamless fit tolerances.
Our standard export packing is engineered for zero-rub container transit: chairs are wrapped in an inner protective breathable non-woven sheet, critical edges and carved legs are shielded with thick shock-absorbing foam profiles, and the entire unit is enclosed in heavy-duty 5-ply double-wall corrugated cartons. Crating or wooden palletization is available for LCL shipments upon request.
Send your project schedule, CAD sketches, target dimension matrix, or reference imagery. Receive an engineered quotation with accurate CBM volume metrics and guaranteed workshop lead times within 24 hours.
